
High-Performance Hydraulic Actuators & Valve Blocks
Engineered to withstand extreme cyclic fatigue, lateral wind sheer, and high surge pressure in mobile cranes, mining trucks, and port machinery.








Evolutionary Trajectory of Boom Luffing Actuation Systems
Deciphering the engineering leap from rudimentary single-acting hydraulic rams to multi-sensor, continuous-feedback derricking power units.
Euler-Bernoulli Column Stability
Boom luffing cylinders represent the ultimate test of hydraulic mechanics. Unlike simple tie-rod cylinders, a luffing cylinder experiences compound dynamic forces: sustained axial compression, immense bending moments caused by wind shear, and sudden inertia shifts during hook load deceleration. Engineering the cylinder rod requires sophisticated Euler column buckling analysis to calculate the exact critical buckling force ($P_{cr}$) across maximum stroke extensions reaching up to 10,000 mm.
HVOF & Laser Cladding Metallurgy
Traditional hard chrome electroplating (0.03–0.05 mm) is progressively failing in marine crane derricking environments due to micro-cracking and galvanic corrosion. Chinese premier manufacturing facilities have standardized on High-Velocity Oxygen Fuel (HVOF) thermal spraying and laser-cladded tungsten carbide (WC-Co-Cr) coatings. These nanostructured barriers deliver micro-hardness exceeding 950–1100 HV0.3 and endure over 1,500 hours in ASTM B117 neutral salt spray tests without pit initiation.
Smart Sensing & Integrated Valving
Modern boom operations require millimeter-level positioning accuracy. By embedding non-contact magnetostrictive linear position sensors inside the hollowed cylinder rod, real-time displacement data is channeled directly to the crane's CAN bus safety system. Direct-flanged overcenter counterbalance valve manifolds guarantee zero load-drift, fail-safe hose-burst locking, and hydraulic anti-cavitation control under negative pulling forces.
Global Sourcing Matrix: Total Cost of Ownership (TCO) vs Failure Risks
A rigorous analytical breakdown for procurement directors navigating the true cost balance between upfront capital expenditure and field warranty liabilities.
| Evaluation Parameter | Legacy Western Sourcing | Low-Tier Low-Cost Producers | China 4.0 Advanced (Micro Precision) |
|---|---|---|---|
| Raw Material Integrity | EN 10083 42CrMo4, certified domestic steel | Commercial St52-3, variable inclusions, porous casting | 42CrMo4 / 30CrMnSiA Electroslag remelted forgings |
| Internal Honing & Ra | Ra 0.2 μm, skived & roller burnished | Ra 0.4–0.6 μm, irregular tool marking, high friction | Ra ≤ 0.1 μm Deep-hole automated skiving burnish |
| Seal Group Architecture | Trelleborg / Parker high-temp polyurethane | Unbranded NBR seals, high stick-slip, early blowout | Trelleborg / Hallite Quad-ring + PTFE step tandem seals |
| Counterbalance Valve Pack | Direct cavity manifold, branded valves | External rigid piping, vulnerable to rupture leaks | Integrated T3A Manifold Zero external pipe joint failure |
| Lead Times & Prototyping | 16 to 26 weeks, rigid revision cycle | 8 to 12 weeks, high variance from drawing | 3 to 5 Weeks Rapid CAD/CAM engineering release |
| Overall TCO Impact | Extremely high CAPEX, stable MTBF | Deceptive CAPEX; catastrophic downtime cost | Optimized TCO 40–55% lower CAPEX with > 99.2% uptime |
China Factory 4.0: Supply Chain Resilience, Metallurgy & Machining Prowess
Inside the engineering core of Qingdao Micro Precision Machinery (MPM): How localized supply integration drives micron-level repeatability.
In-House Closed-Loop Machining Ecosystem
From our 3,500 m² heavy-machining facility in Chengyang District, Qingdao, MPM controls 100% of the machining envelope. Heavy boom luffing cylinders require stringent concentricity between the cylinder barrel bore, the gland threads, and the trunnion pivot eye. By consolidating CNC turning, horizontal multi-axis milling, and high-load grinding under one roof, our facility holds concentricity within 0.02 mm.
Our tooling division manufactures its own ER collet chucks, DIN 69872 retention knobs, and specialized tool holders—a unique vertical integration ensuring zero chatter marks on cylinder gland internal threads and seal grooves.
Metallurgical Quality Assurance & Cleanliness
Hydraulic seal extrusion, oil blistering, and premature scoring are predominantly traced back to micro-particulate contamination and metallographic inclusions in the cylinder barrel raw tube. MPM sources heavy-wall cold-drawn seamless tubing adhering to strictly verified metallurgical chemistry: carbon content controlled within 0.38–0.45% and trace sulfur kept below 0.015% to eliminate hot-shortness during heavy friction welding.
Every single cylinder is washed through an automated high-pressure multi-stage ultrasonic chamber. Flushing fluid is tested in our laboratory to certify fluid cleanliness to ISO 4406 Cleanliness Level 16/14/11 before assembly and final electrostatic protective coating.
Global Industrial Deployment & Application Sectors
Analyzing operating stress profiles across heavy engineering, maritime lifting, tunneling, and high-cycle material handling infrastructure.
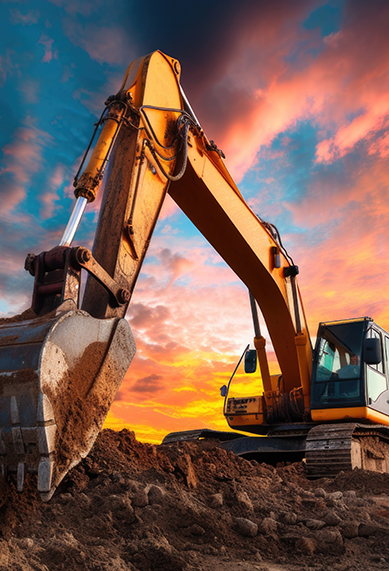
High-Tonnage Heavy Excavators
Excavator boom actuators experience continuous cyclic pressure spikes up to 38 MPa as the bucket encounters subterranean granite. MPM end-cushioned designs attenuate return shock waves by 40%, protecting pin bushes and structure welds.
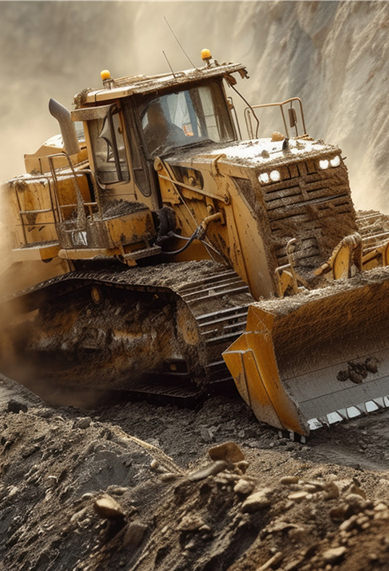
Backhoe & Wheel Loaders
Continuous loading cycles require minimal hysteresis and superior low-friction seals. MPM cylinders utilize composite guide rings with graphite impregnation to eliminate stick-slip jitter during micro-adjustments.
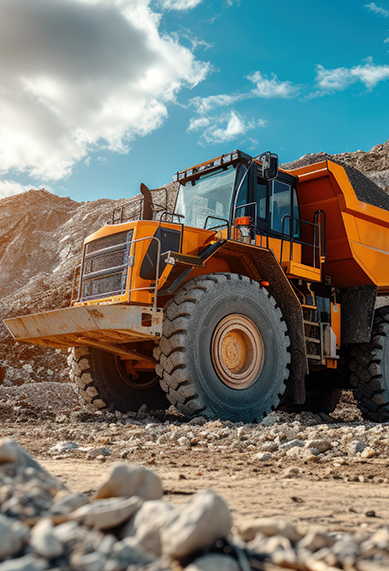
Heavy Forklifts & Reach Stackers
Handling 40-foot intermodal containers demands synchronous double-acting luffing cylinders with zero internal bypass leakage. Machined with ISO 6H class precision nuts and precision-matched pistons.
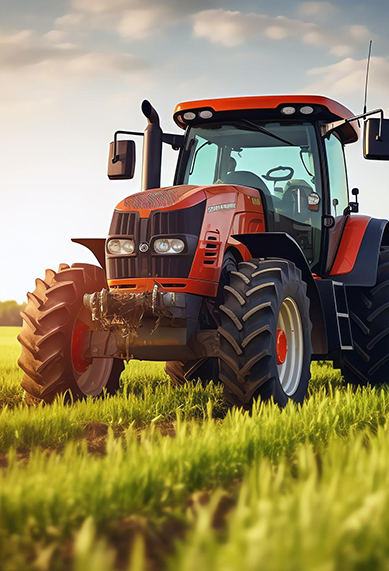
Reversible Ploughs & Harvesters
Engineered to operate in dense abrasive dust and corrosive agro-fertilizer vapors. Features secondary viton scraper seals and nitride-quenched rod surfaces to ensure zero seasonal breakdown.
Parametric Design Boundaries for Boom Luffing Actuation
A reference checklist for fluid power engineers specifying custom luffing cylinders for mobile lattice and telescopic booms.
Bore & Rod Proportions
Because luffing cylinders encounter extreme compressive loads during boom raising and significant tensile tensile drag during steep boom lowering, rod ratios typically range between 1.4:1 and 1.8:1. A large-diameter chrome rod maximizes the moment of inertia ($I = \frac{\pi d^4}{64}$), actively preventing middle-section deflection under heavy wind.
Spherical Bearing Geometry
Deflections in long crane booms induce high angular misalignments at the trunnion and rod-end pins. Standard rigid bushings cause edge-loading, destroying rod seals within hundred operating hours. MPM incorporates maintenance-free, self-lubricating PTFE composite or high-strength copper alloy spherical plain bearings with greasing channels.
Cushioning Dynamics at Ends
Decelerating a 40-meter multi-section crane boom requires controlled progressive pressure buildup. Our patented floating cushion collars introduce non-linear fluid throttles over the final 50 mm of stroke, preventing destructive pressure spikes while allowing rapid acceleration in the reverse direction via integrated check valves.
Frequently Asked Questions: Sourcing Hydraulic Actuators from China
Direct technical answers addressing engineering interchangeability, seal compatibility, burst testing, and reverse engineering.
What specific parameters are mandatory to calculate Euler buckling limits for custom luffing cylinders?
Can Micro Precision Machinery reproduce legacy OEM crane cylinders from worn physical samples?
How does an integrated counterbalance (overcenter) valve prevent uncontrolled boom dropping?
Which surface coating offers the best return on investment for maritime and harbor crane cylinders?
What testing procedures are performed before overseas shipment from your Qingdao plant?
How do you guarantee batch-to-batch consistency for hydraulic manifold valve blocks?
Specialized Boom Cylinders, Bases & Kinematic Linkages
Comprehensive mobile hydraulic components manufactured to rigorous ISO/DIN industrial standards.








Collaborate with Qingdao Micro Precision Engineers
Submit your CAD drawings (.DWG, .STEP, .PDF), operational parameters, or OEM part numbers. Our technical team responds within 24 hours with comprehensive FEA reviews, dimensional tolerance verification, and transparent volume quotations.